Industrial-Grade Glass Packaging Engineering, Custom Color Synthetics, and High-Throughput Bulk Supply Chains Tailored for Noro and Pacific Maritime Hubs
Send Inquiry NowHigh-precision amber, black, frosted, and custom-painted glass bottles optimized for spirit distillers, pharmaceuticals, and commercial beverage bottlers in Noro.
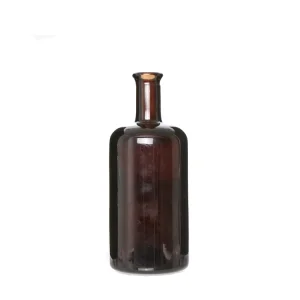
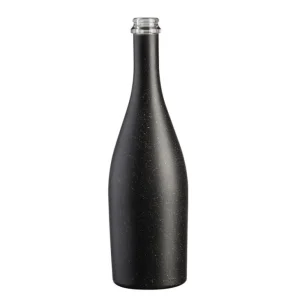
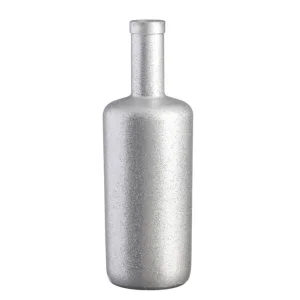
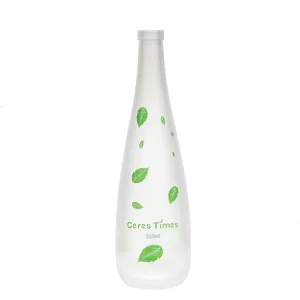
End-to-end glass design, molding, and high-efficiency manufacturing capabilities supplying Noro's expanding industrial base.


Strategic Insights, Photoprotective Material Science, and Macro Logistics Solutions for Western Province Enterprises
As the commercial and industrial heart of Solomon Islands' Western Province, Noro has rapidly evolved into a critical maritime hub for processing, bottling, and export logistics. The regional growth in artisanal spirit distillation, beverage processing, premium oil extractions, and commercial tuna/agri-product sub-industries has created a sophisticated demand for robust, high-performance glass packaging. In humid tropical environments like Noro, glass packaging must not only serve as a brand differentiator but also fulfill stringent chemical inertness, UV radiation barrier protection, and mechanical resilience requirements during oceanic transit.
This whitepaper outlines the technical parameters, structural advantages, and procurement strategies for sourcing colored glass bottles (Amber, Cobalt Blue, Antique Green, Matt Black, and Custom Screen-Printed variants) optimized for enterprise buyers operating in Noro and across the South Pacific corridor.
Exposure to high solar ultraviolet indices in tropical port zones can drastically degrade light-sensitive organic compounds in beverages and liquids via photo-oxidation. Sourcing high-density colored glass (specifically amber with iron oxide enrichment or specialized external UV coatings) extends product shelf-life by up to 300% compared to standard clear flint glass.
Colored glass manufacturing requires absolute thermal precision and rigorous stoichiometric control of transition metal oxides within the glass matrix. Our self-owned manufacturing facilities utilize advanced IS (Individual Section) machines and automated batching systems to achieve consistent optical density and mechanical durability.
Synthesized via carbon and sulfur additions to iron-rich silica formulations. Yields maximum spectral filtration between 300nm and 450nm, rendering it ideal for botanical spirits, craft beers, and pharmaceuticals sensitive to light degradation.
Formulated using high-purity Cobalt Oxide ($CoO$) and Chromium Oxide ($Cr_2O_3$). Delivers luxury aesthetic value while providing moderate photoprotection for super-premium vodkas, gins, and specialized oils.
Secondary processing using organic electrostatic spraying, thermal curing, and acid etching. Produces matte black, tactile frost, and high-impact custom gradient finishes resistant to scratching and humidity degradation.
Shipping high-density glass packaging across Pacific trade routes demands rigorous packaging engineering to prevent thermal shock breakage, micro-fracturing, and ocean freight moisture damage. Our supply chain protocols for shipments arriving at Noro Port include:
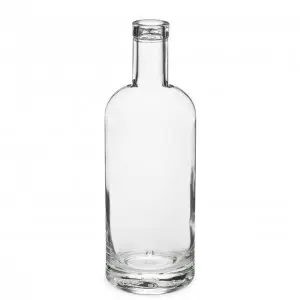
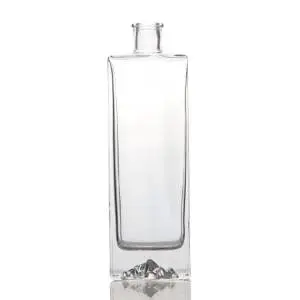
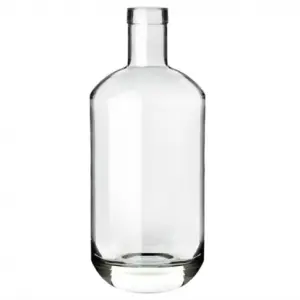
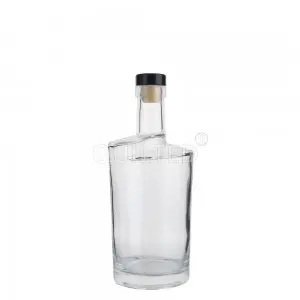
In Stock, On Time: QLT Glass, Your Swift Solution for Premium Packaging. Ready to Ship Excellence!
Decarbonization, Lightweighting, and Advanced Optical Decoration Techniques
Through Narrow Neck Press and Blow (NNPB) machinery, we reduce total glass weight by up to 20% while maintaining structural wall thickness and burst strength ($\ge 1.4\text{ MPa}$). This significantly decreases container shipping freight costs to Pacific destinations such as Noro Port.
Our ceramic printing and screen decoration lines strictly utilize eco-friendly, heavy-metal-free thermosetting inks compliant with FDA 21 CFR, EU 1935/2004, and local Solomon Islands environmental protection parameters.
As a leading Chinese glass bottle manufacturer, we take pride in our ability to produce glass bottles from start to finish. Our integrated processes encompass raw material crushing and mixing, precise batching, melting in energy-optimized furnaces, automated shaping, and meticulous annealing, ensuring top-notch quality at every step of production.
Explore our full range of 350ml, 500ml, 700ml, 750ml, and 1000ml colored and extra-flint bottles engineered for global compliance.
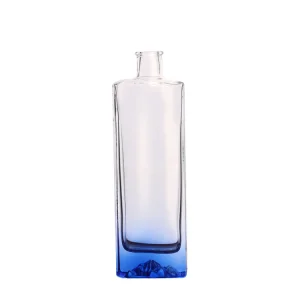
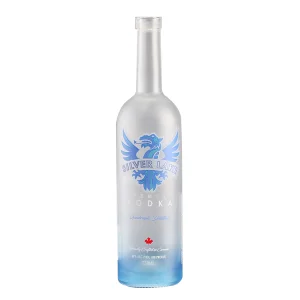
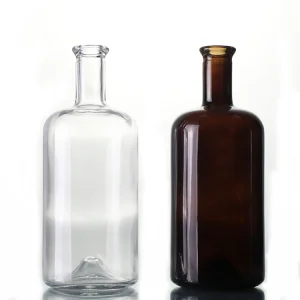
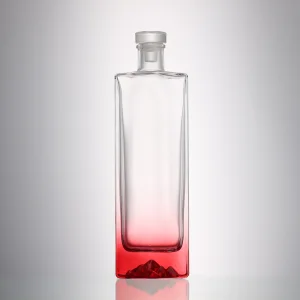
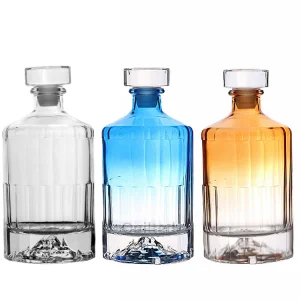
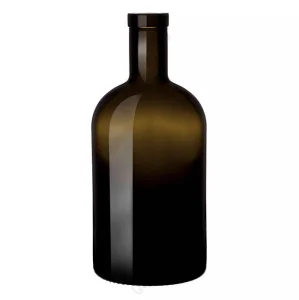
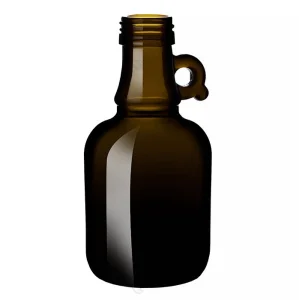
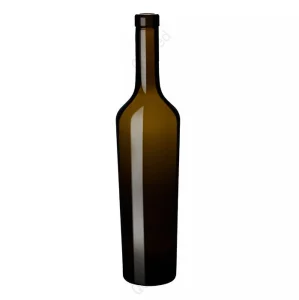
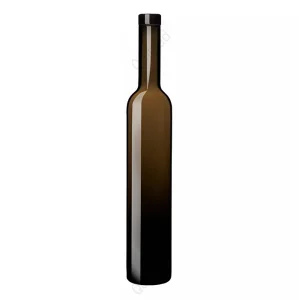
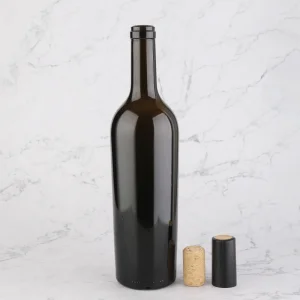
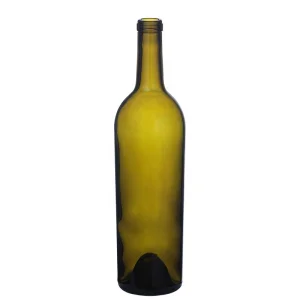
Complete glass bottling solutions manufactured under strict ISO quality systems for global spirit, wine, and beverage brands.
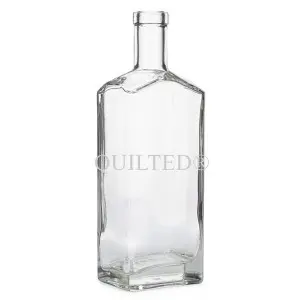
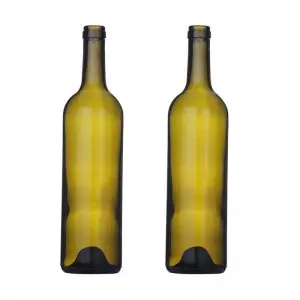
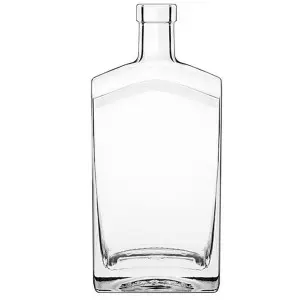
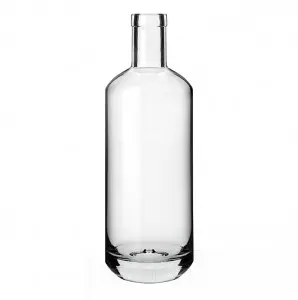
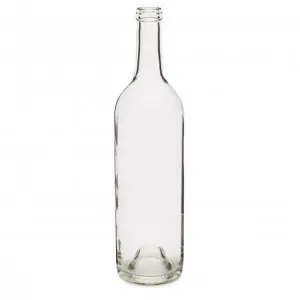
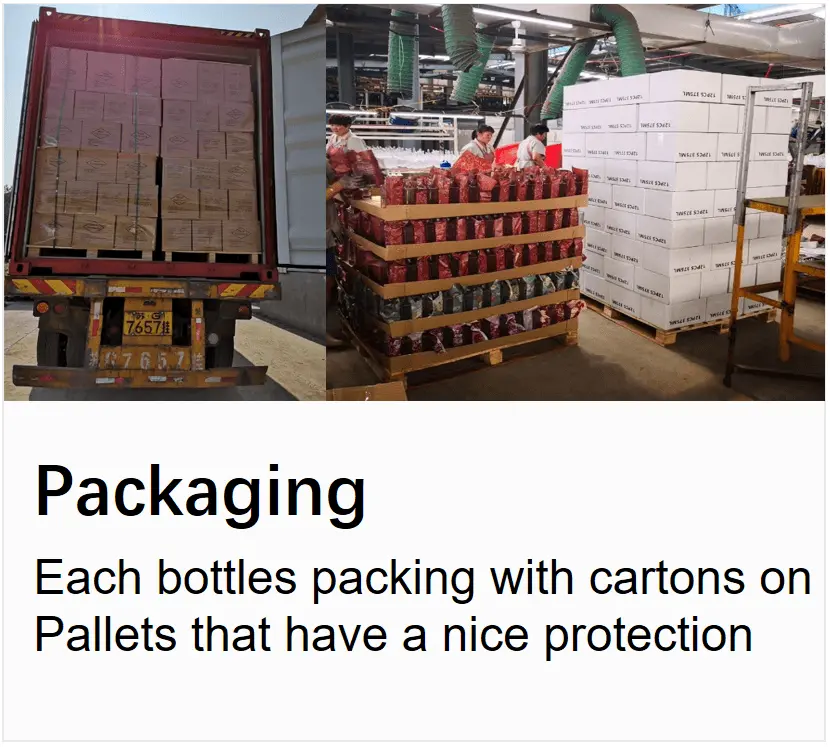
Expert insights regarding shipping, custom mold development, UV protection, and bulk procurement to Noro and Pacific destinations.
Partner with a trusted, vertically integrated glass manufacturer. Contact our engineering team today for instant quotes, technical specifications, and complimentary samples.
Send Inquiry Now QLT Glass